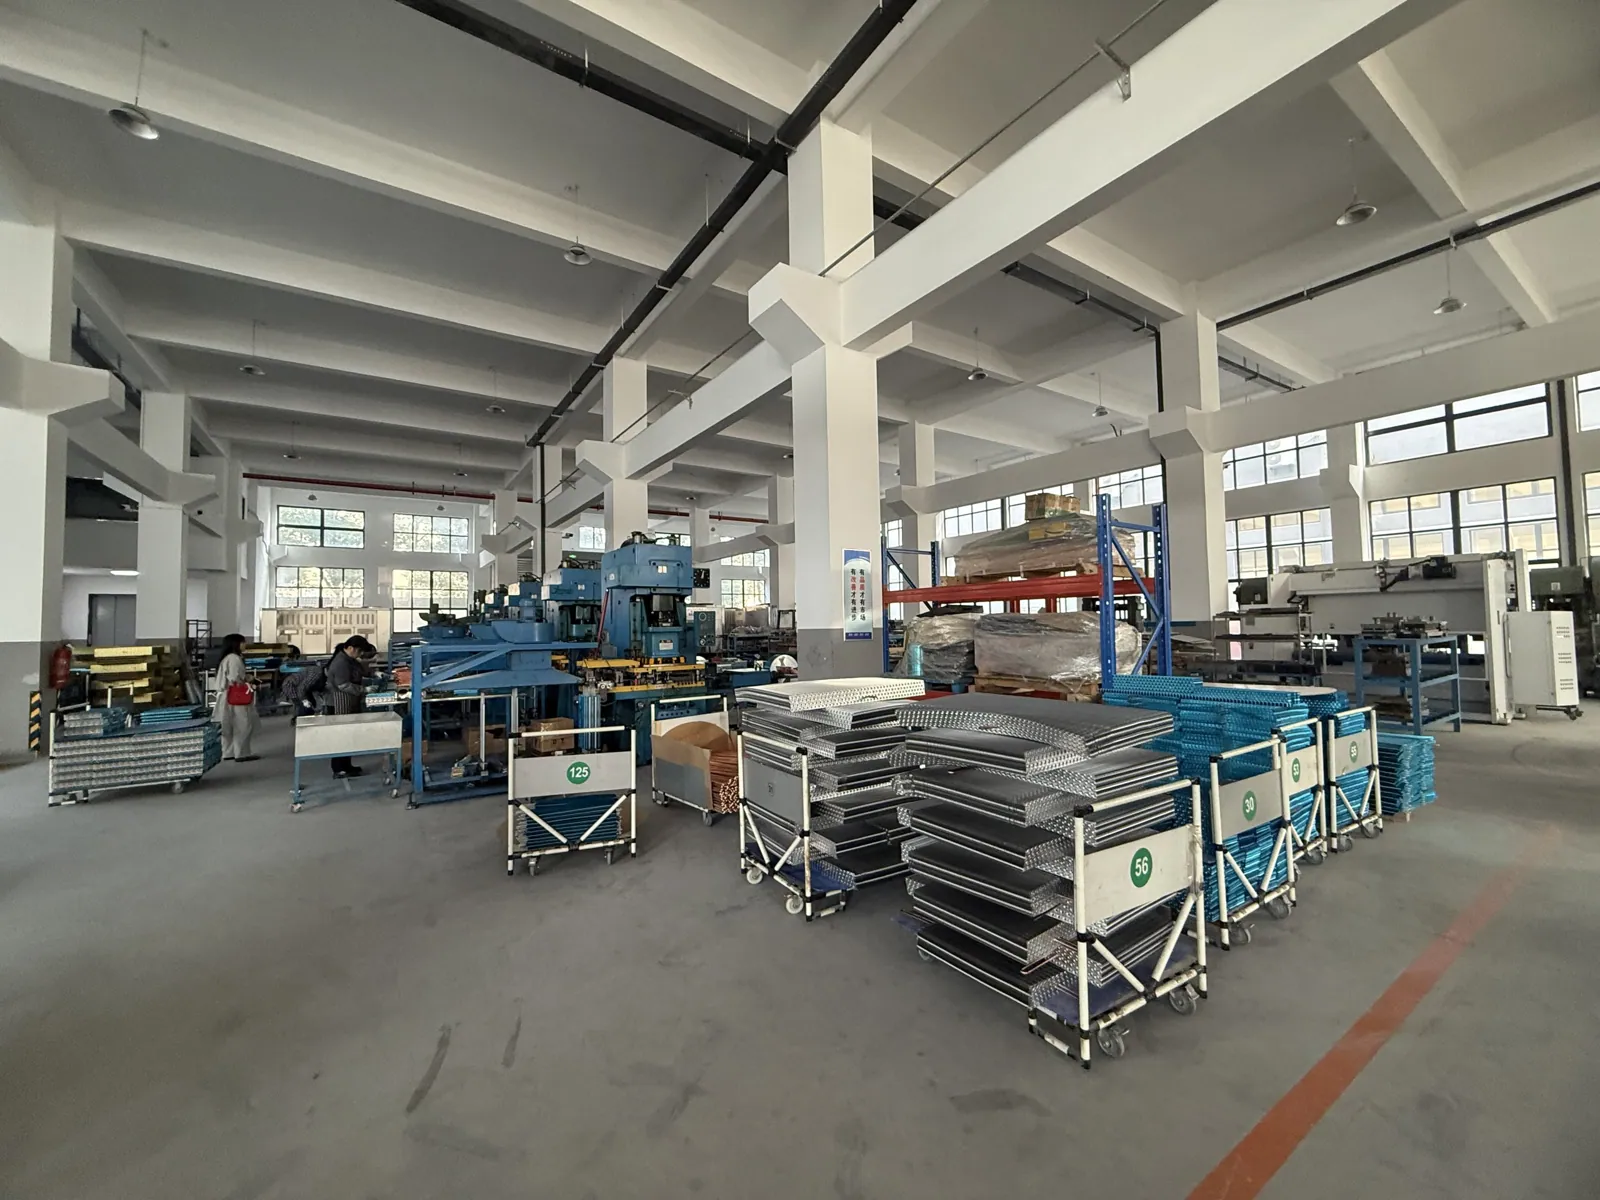
Heat exchanger workshop at the Lemosun plant in Ningbo

Capabilities

A 12,000 m² plant in Jiangbei District, Ningbo, with 105 people. Below is the route a heat exchanger takes through it, photographed as it happens.

How a coil is made

Eleven stages, from a reel of copper tube to a packed coil on a pallet.

  1. 01

    Tube bending

    Copper tube is uncoiled, straightened, cut and bent into hairpins.
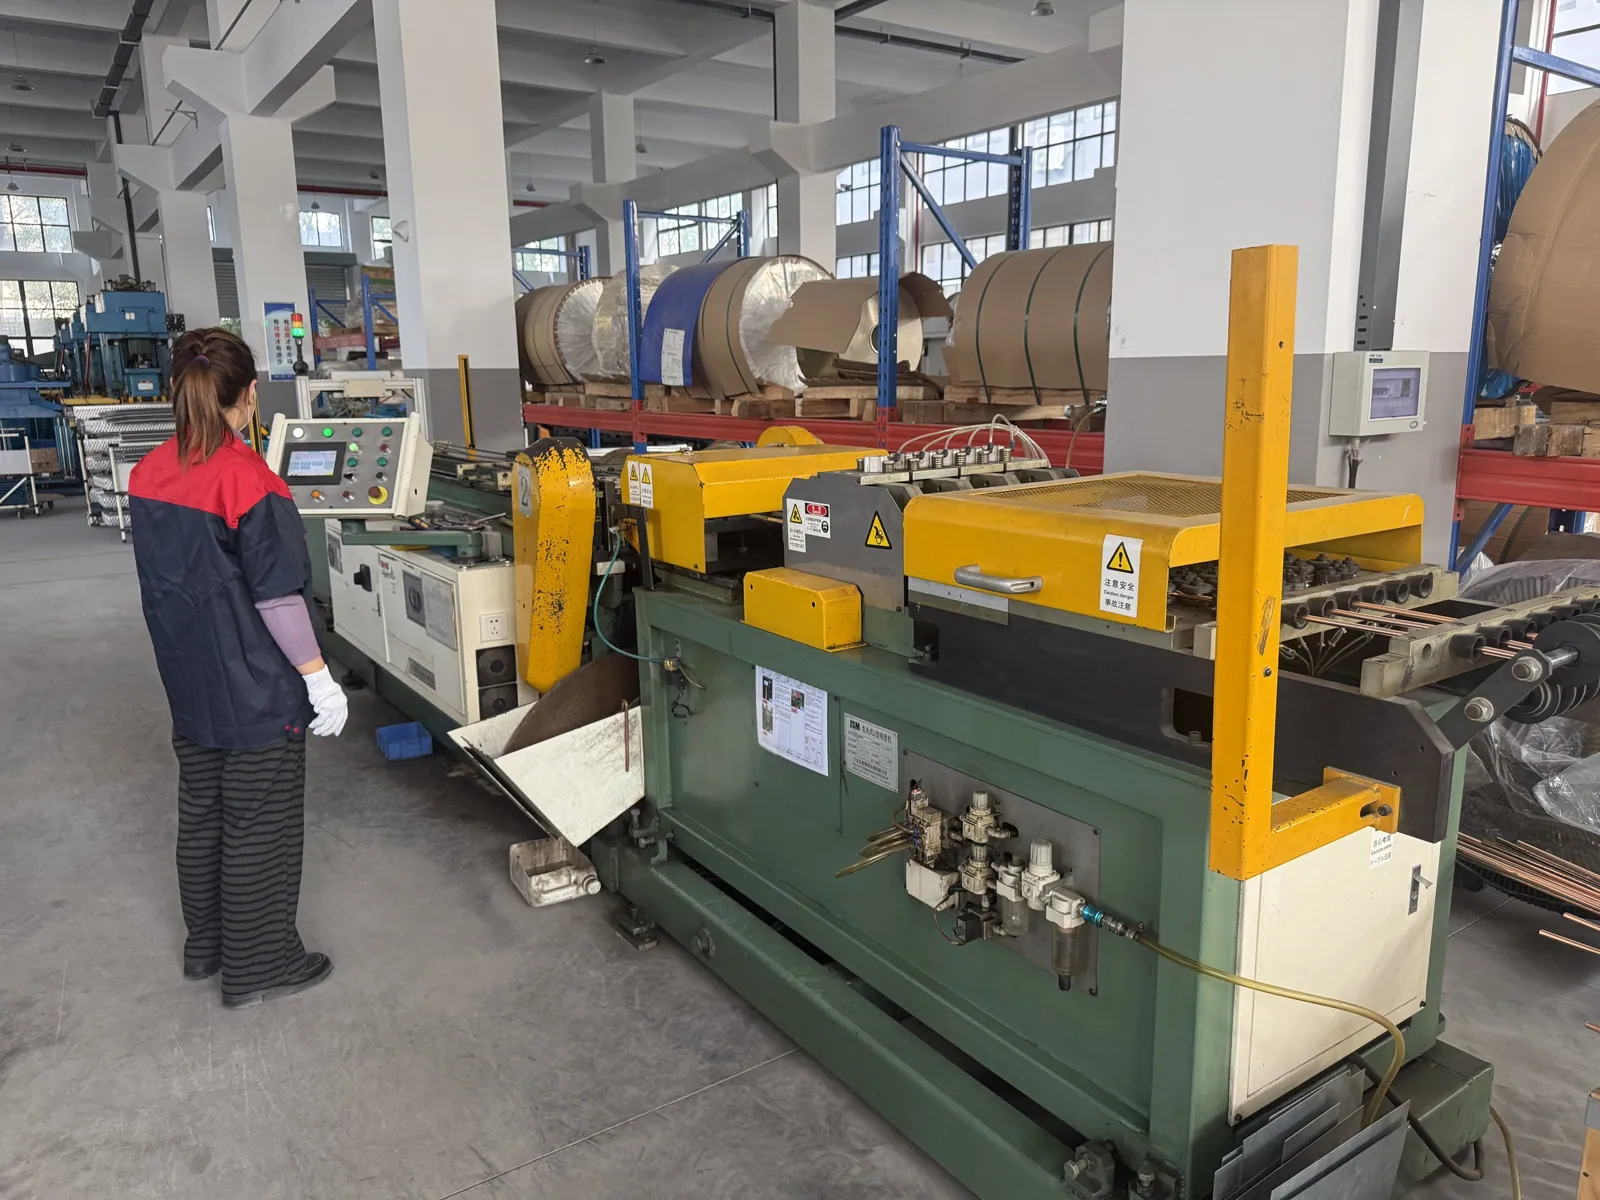
    Operator at the copper tube hairpin bending machine
  2. 02

    Fin stamping

    A press line stamps the fin pattern and collars into aluminum foil at the pitch on the drawing.
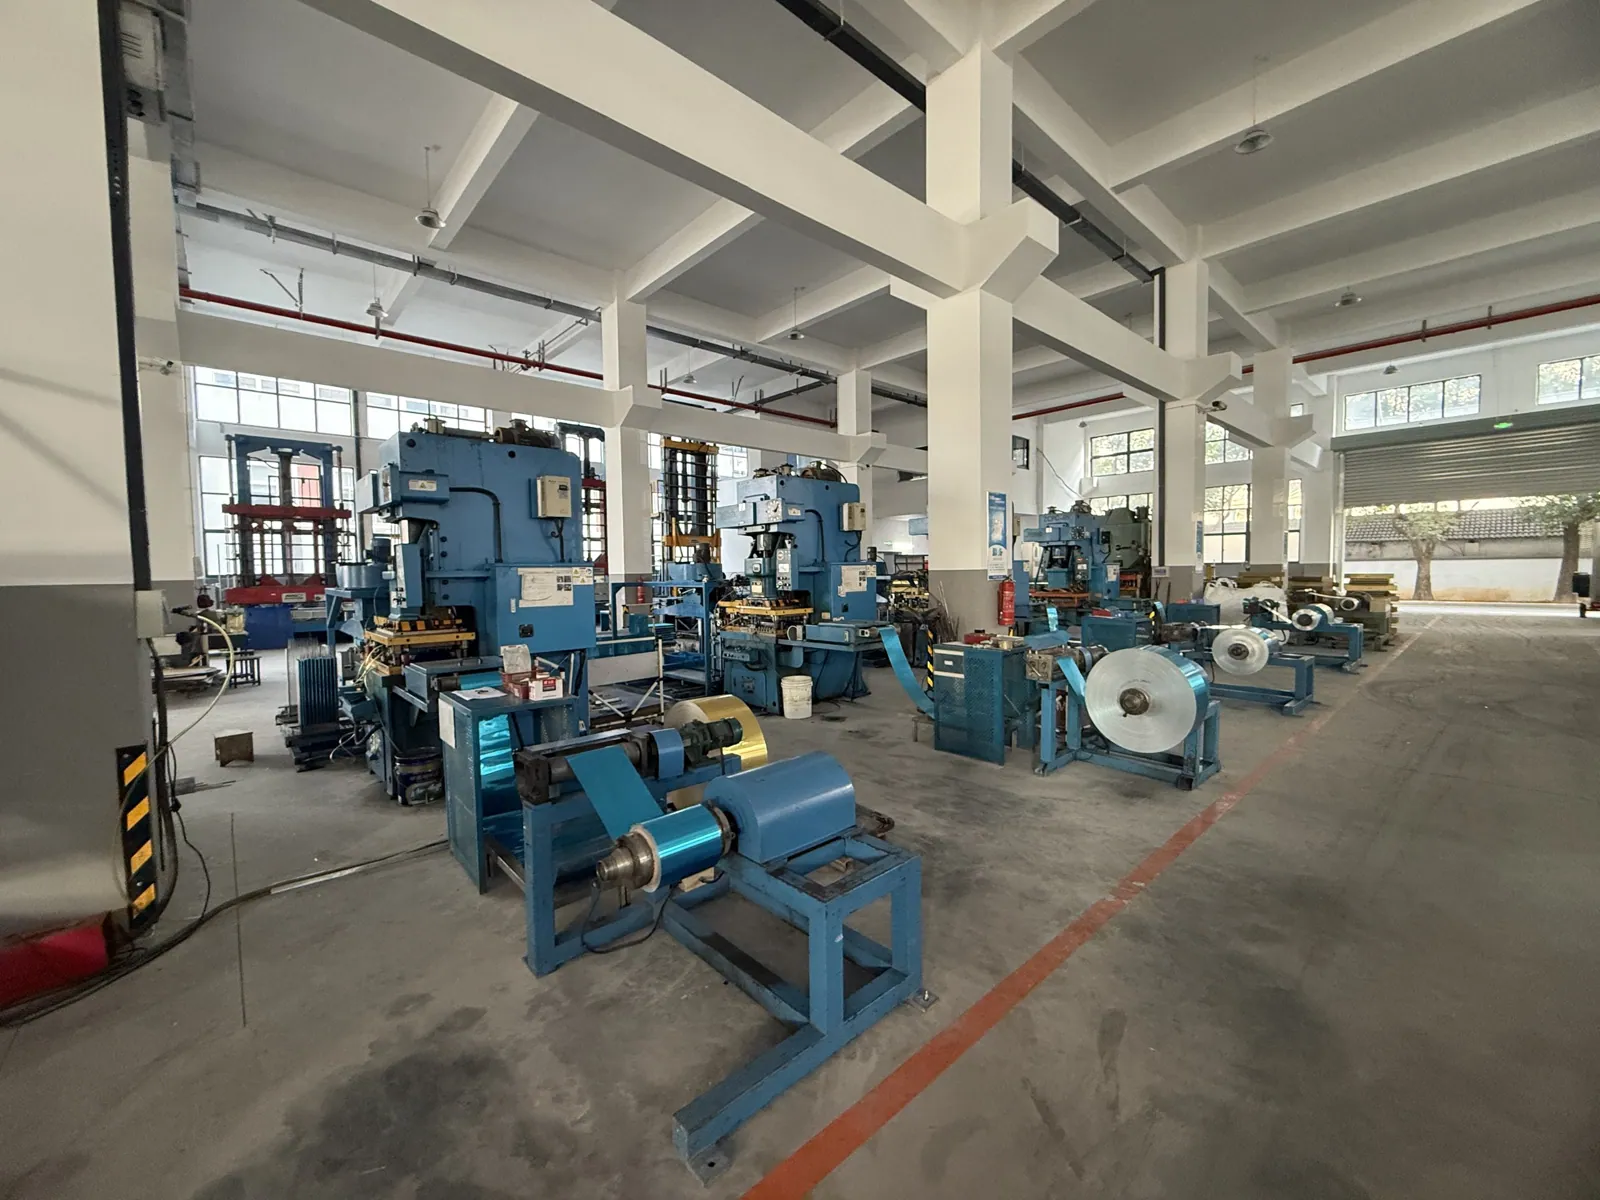
    Aluminum fin stamping press line
  3. 03

    Fin insertion

    Hairpins are laced through the fin stack by hand and the tube count is checked.
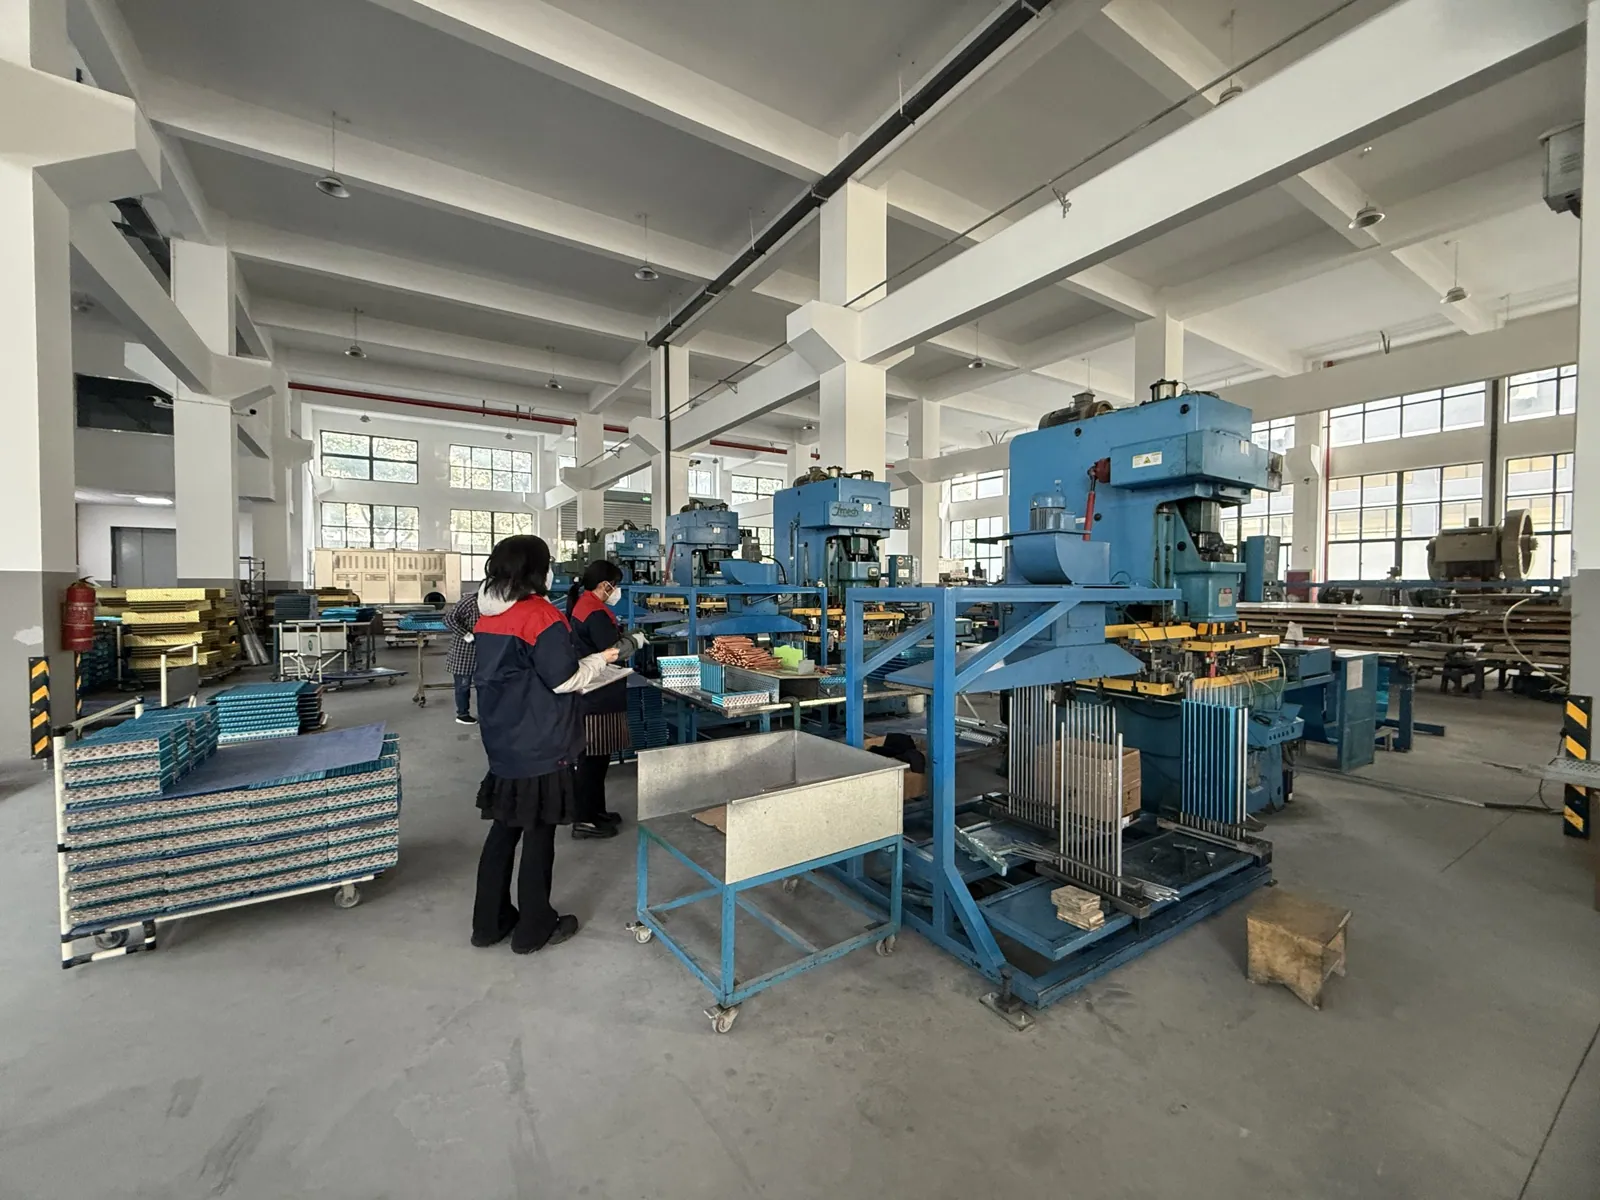
    Workers lacing copper hairpin tubes through aluminum fins
  4. 04

    Tube expansion

    The tubes are expanded mechanically so that they press against the fin collars.
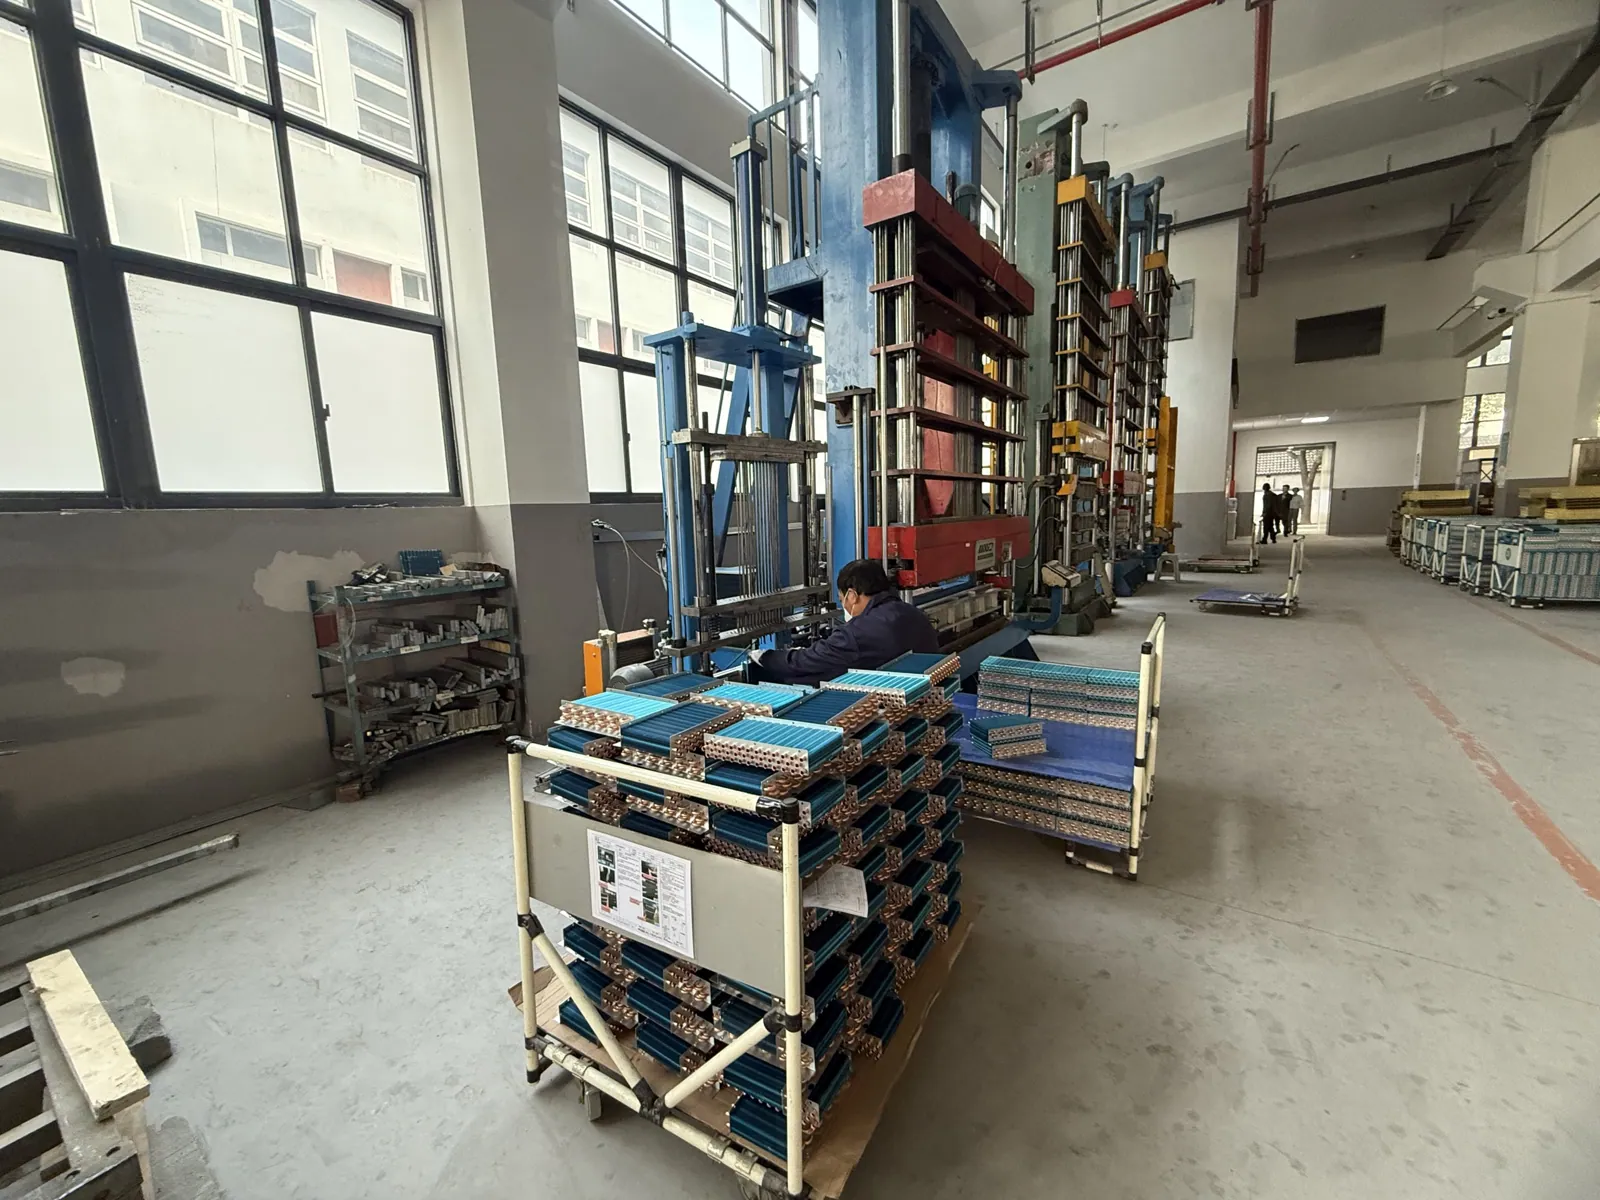
    Vertical tube expansion machine with a heat exchanger coil
  5. 05

    Cleaning and drying

    Oil from stamping and expansion is removed and the coil is dried in an oven.
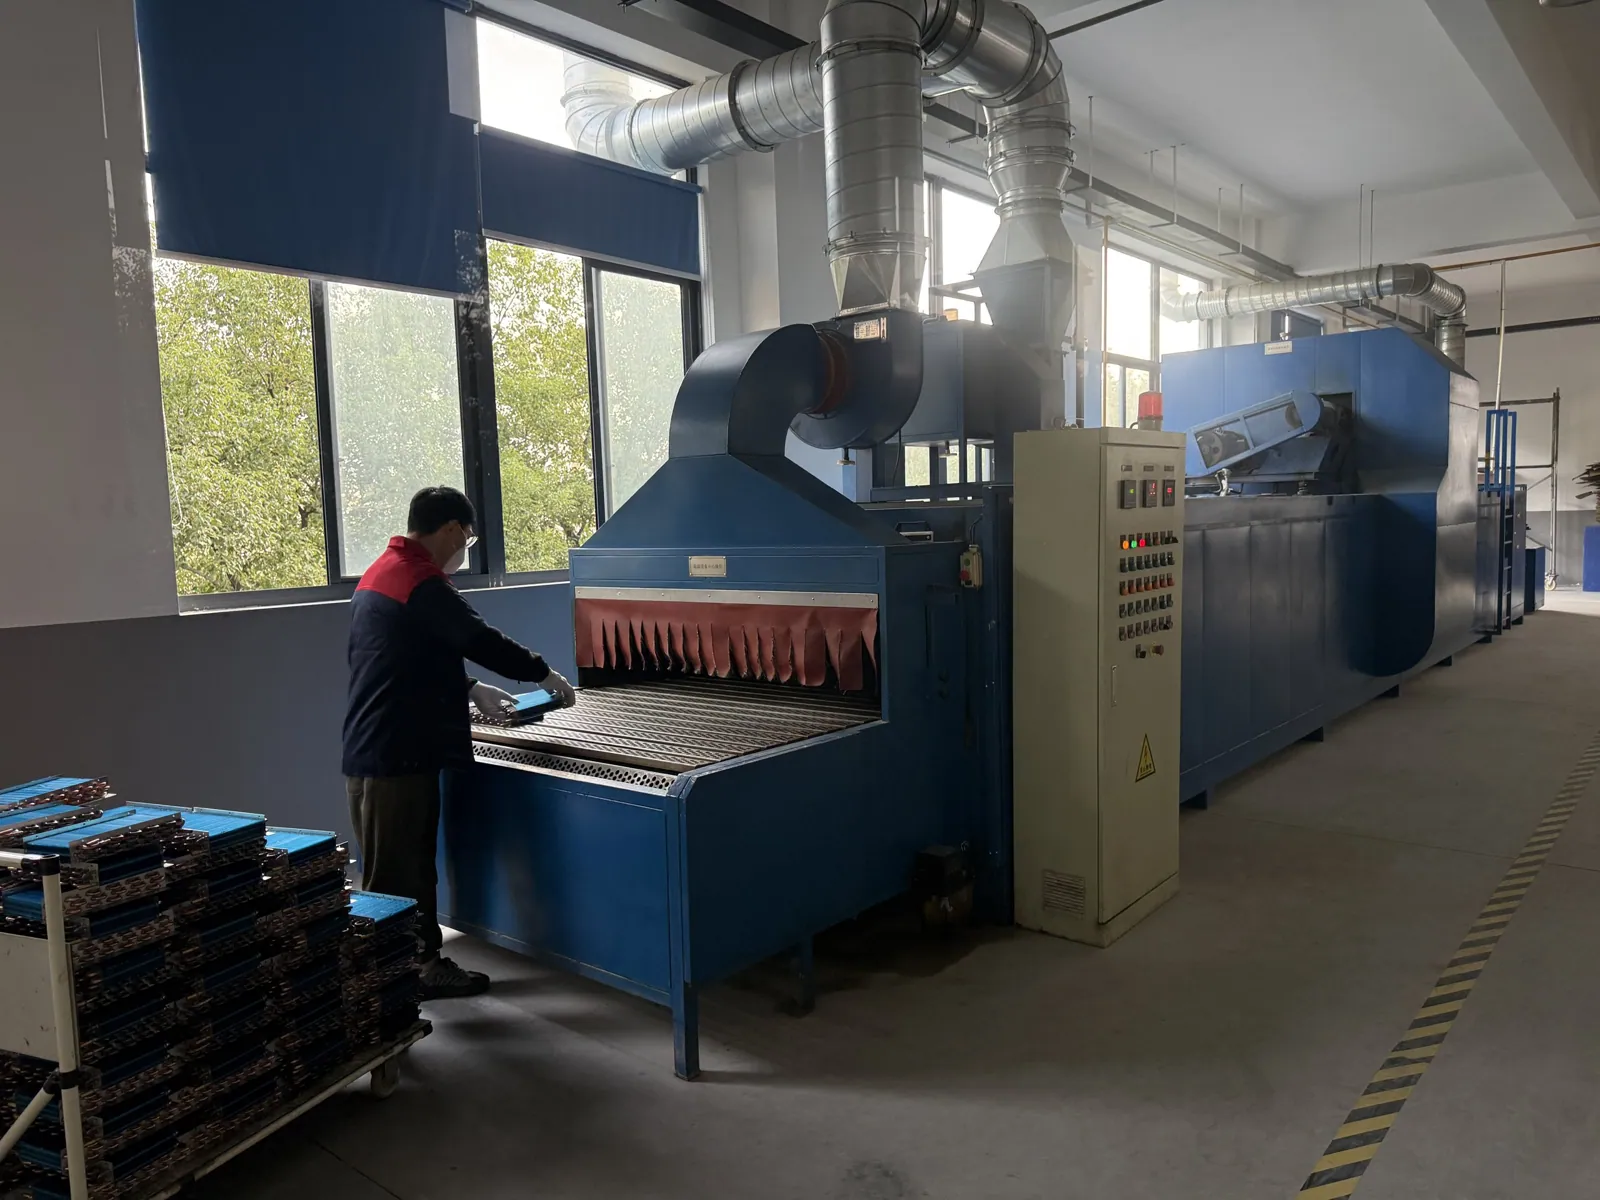
    Drying oven line for heat exchanger coils
  6. 06

    Coil bending

    Where the drawing asks for it, the flat coil is bent into an L or U shape.
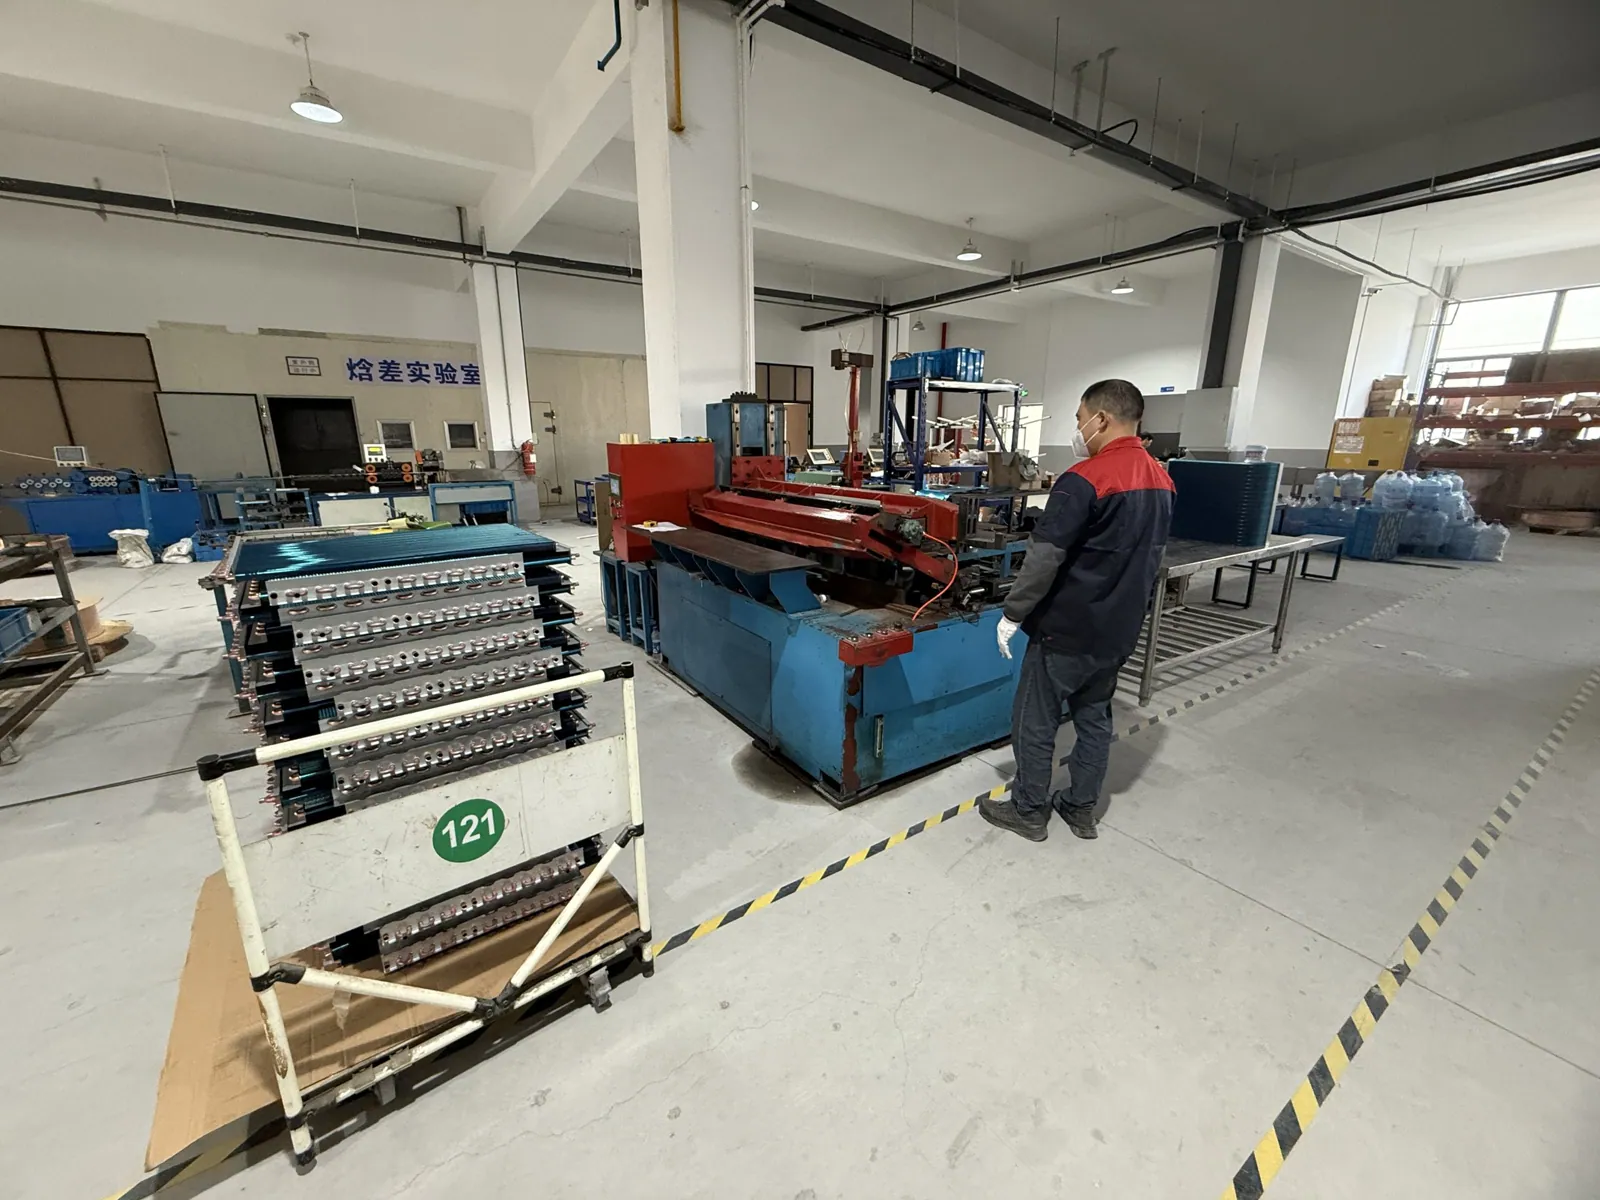
    Coil bending machine forming a finned heat exchanger
  7. 07

    Brazing

    Return bends and headers are brazed to close the refrigerant circuits.
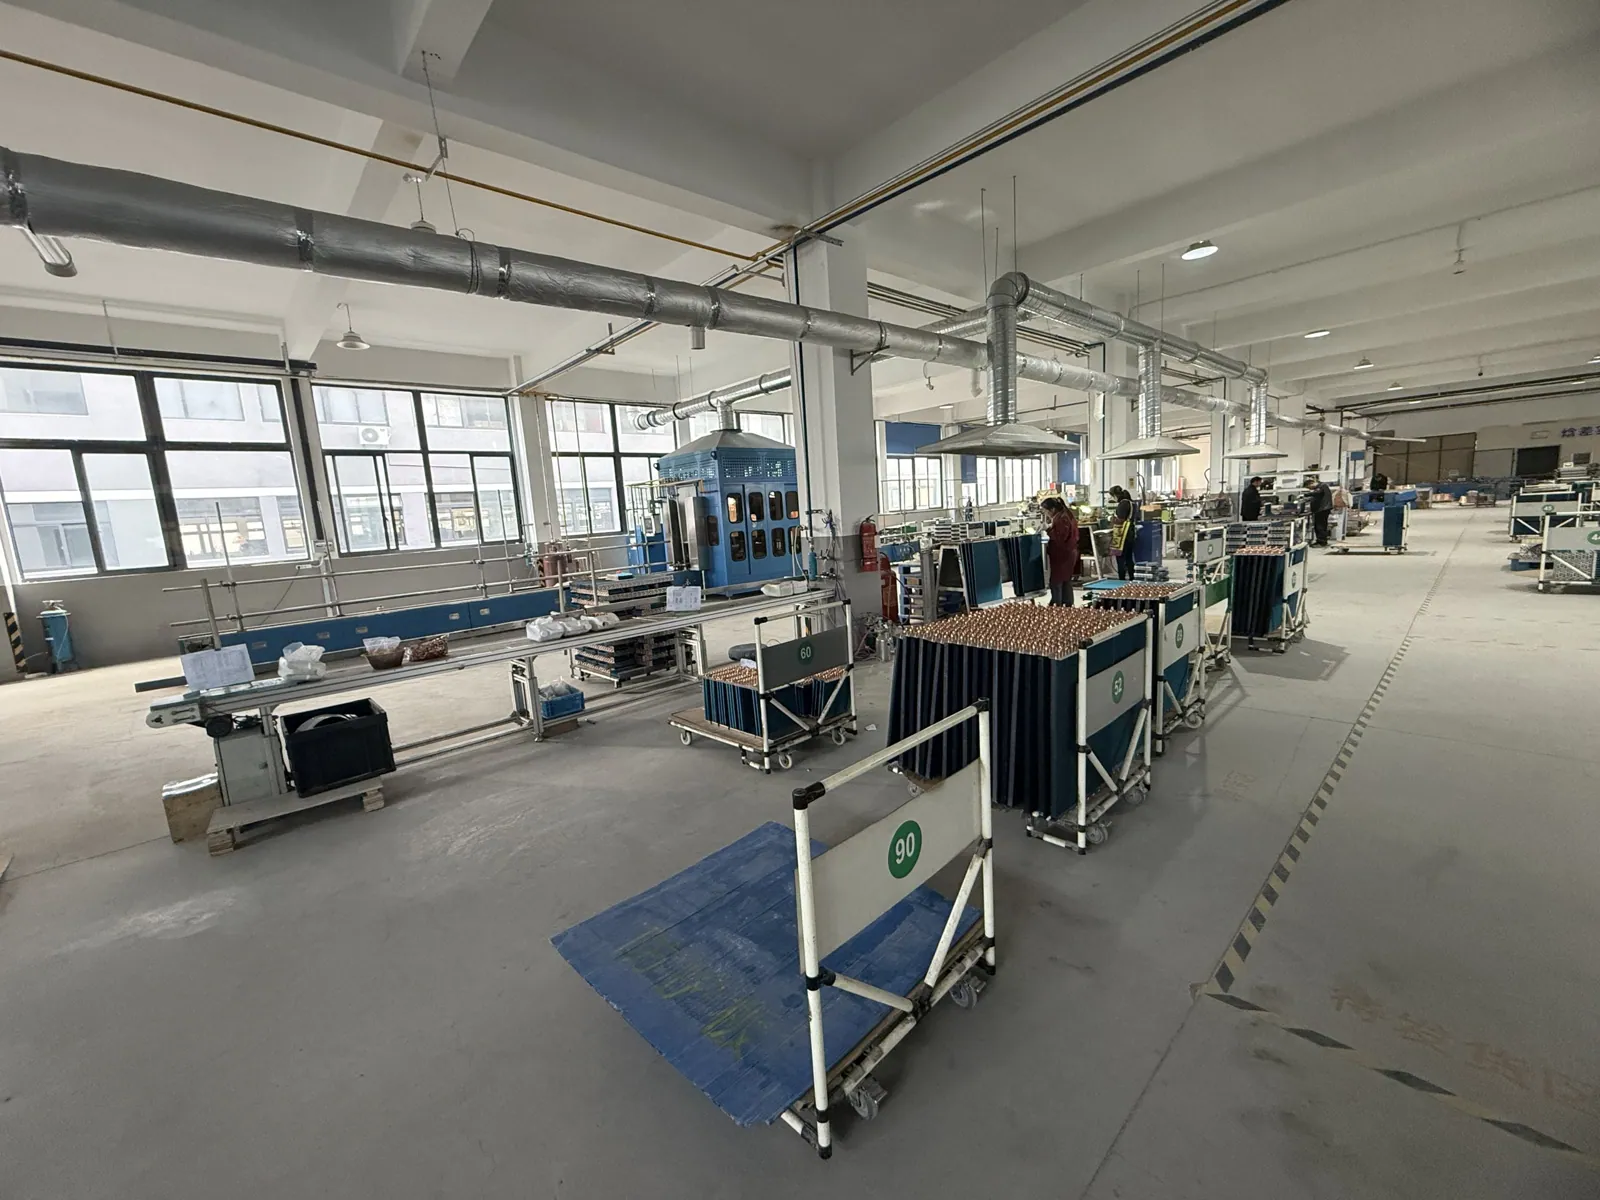
    Technician brazing copper return bends on a heat exchanger
  8. 08

    Leak testing

    Every coil is pressurized to 3.8 MPa and checked for leaks.
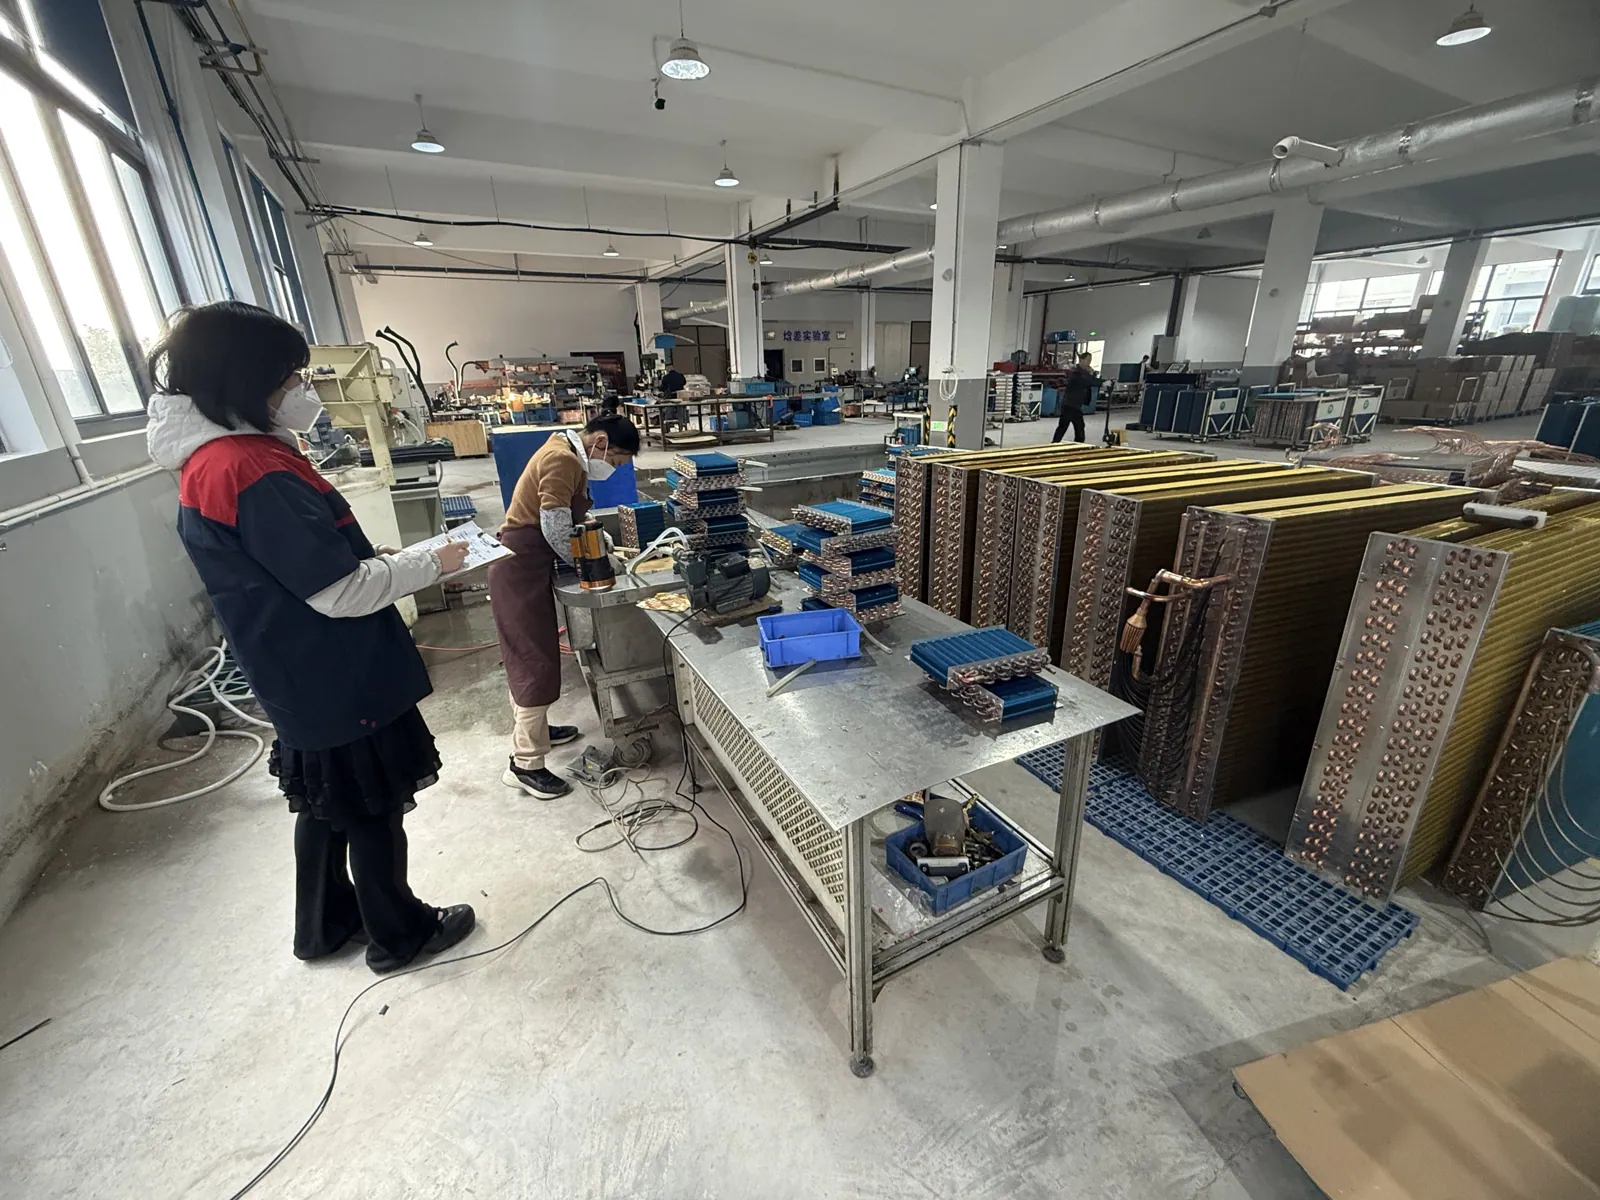
    Heat exchanger coil under pressure in the leak test station
  9. 09

    Final inspection

    Inspectors check finished units and record the results.
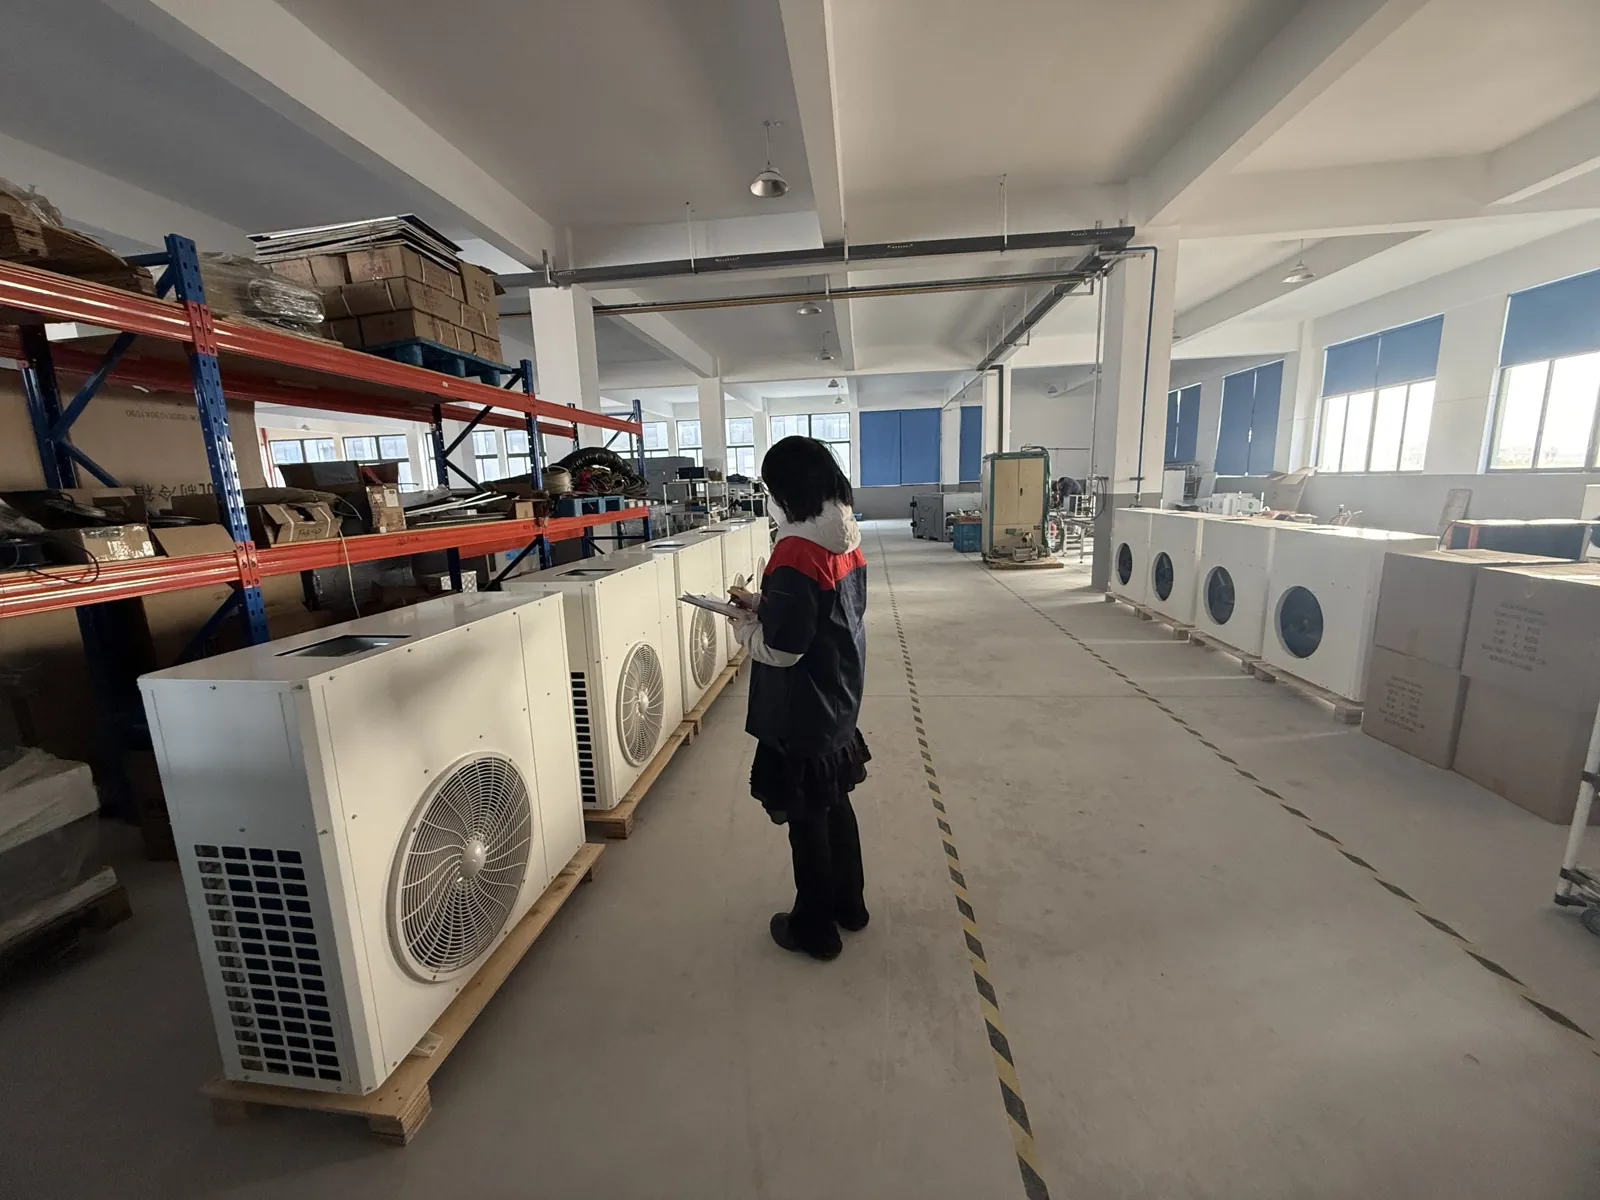
    Inspectors checking finished units on the line
  10. 10

    Packing

    Coils and units are protected and packed for export.
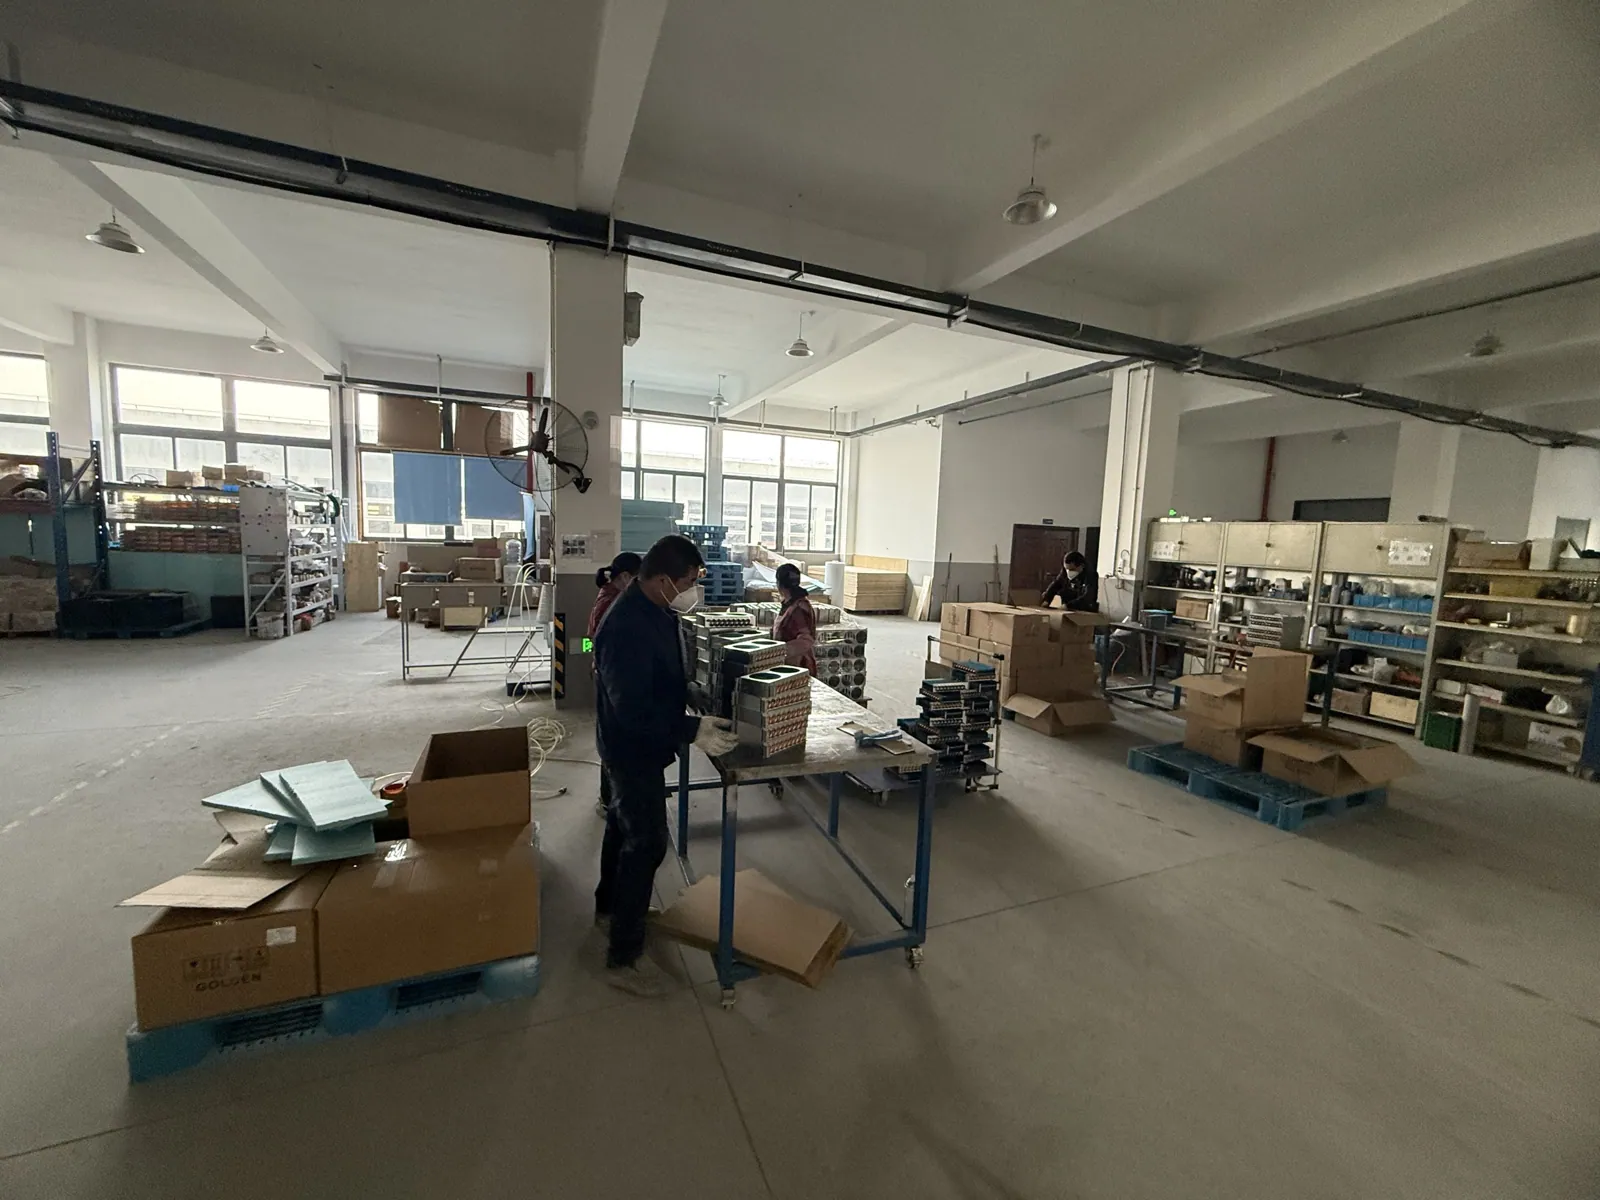
    Packing area with finished products in cartons
  11. 11

    Ready to ship

    Packed goods wait in the dispatch area for loading.
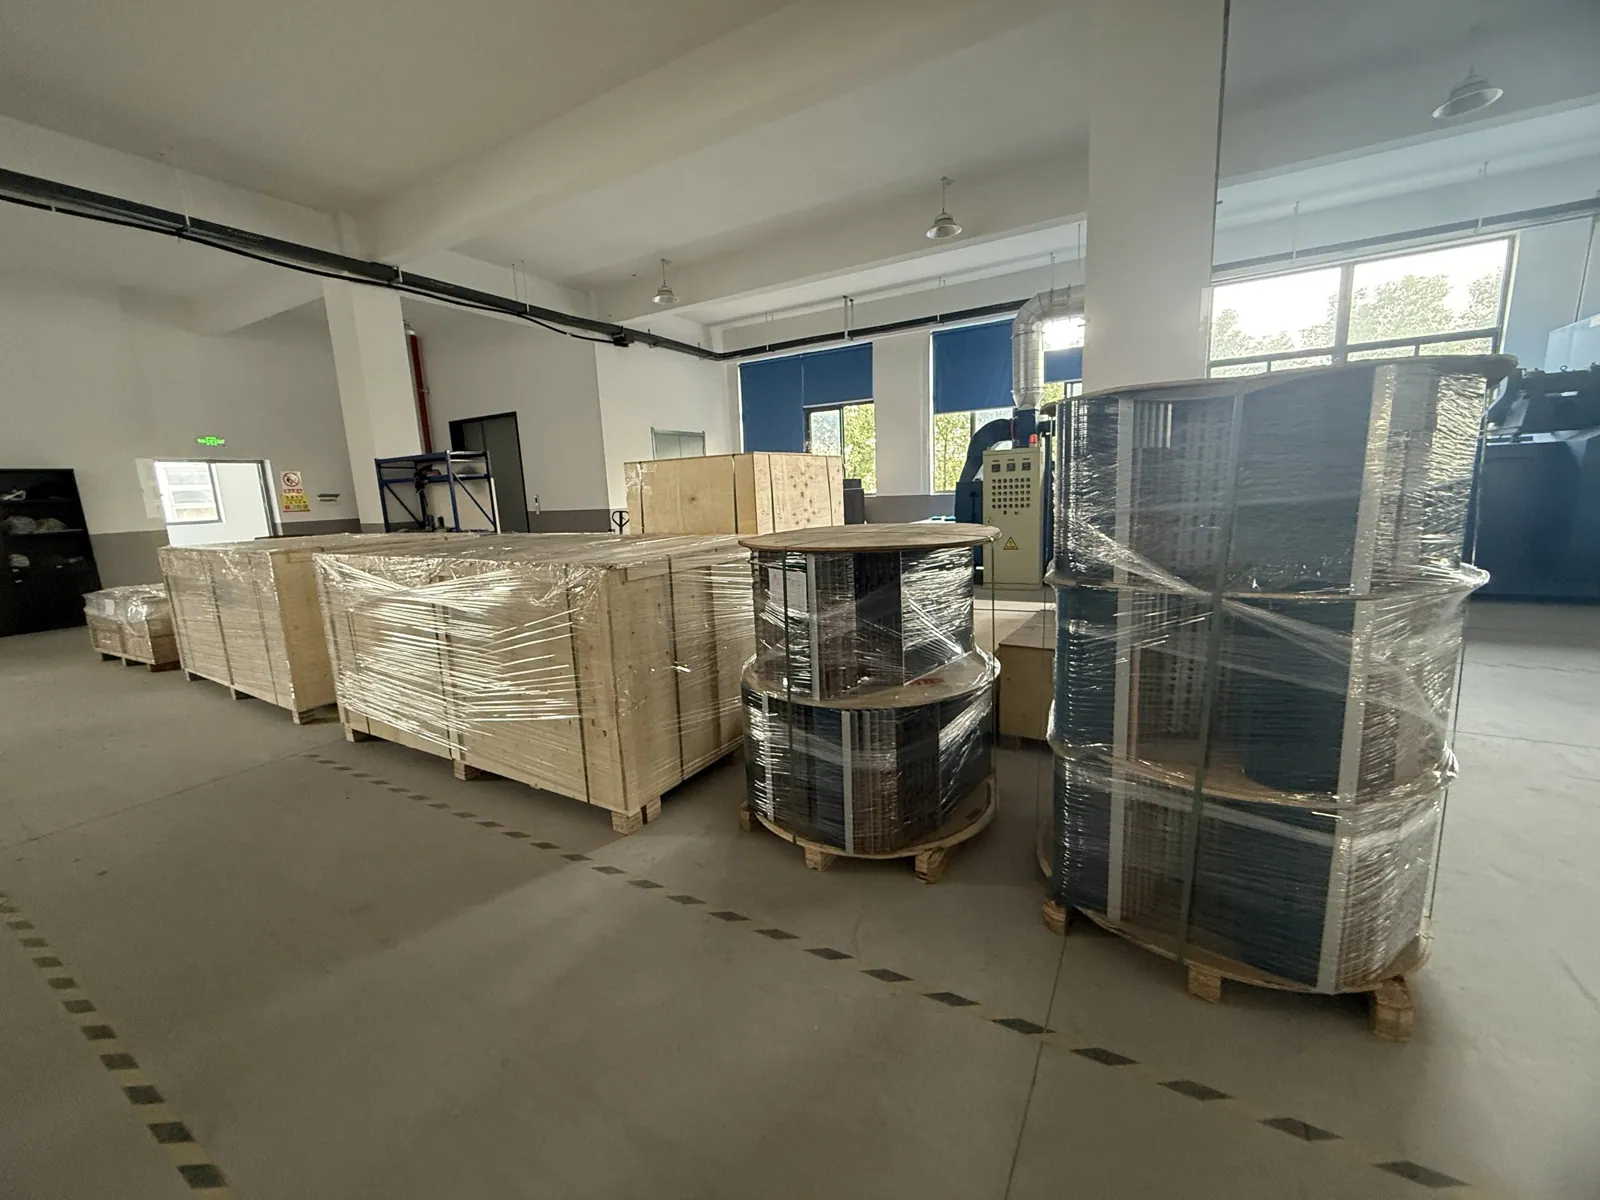
    Packed goods on pallets ready for shipment

Between brazing and packing, coils are also blown clean with air and the fins are combed straight.

What goes in

The two materials every coil starts from.
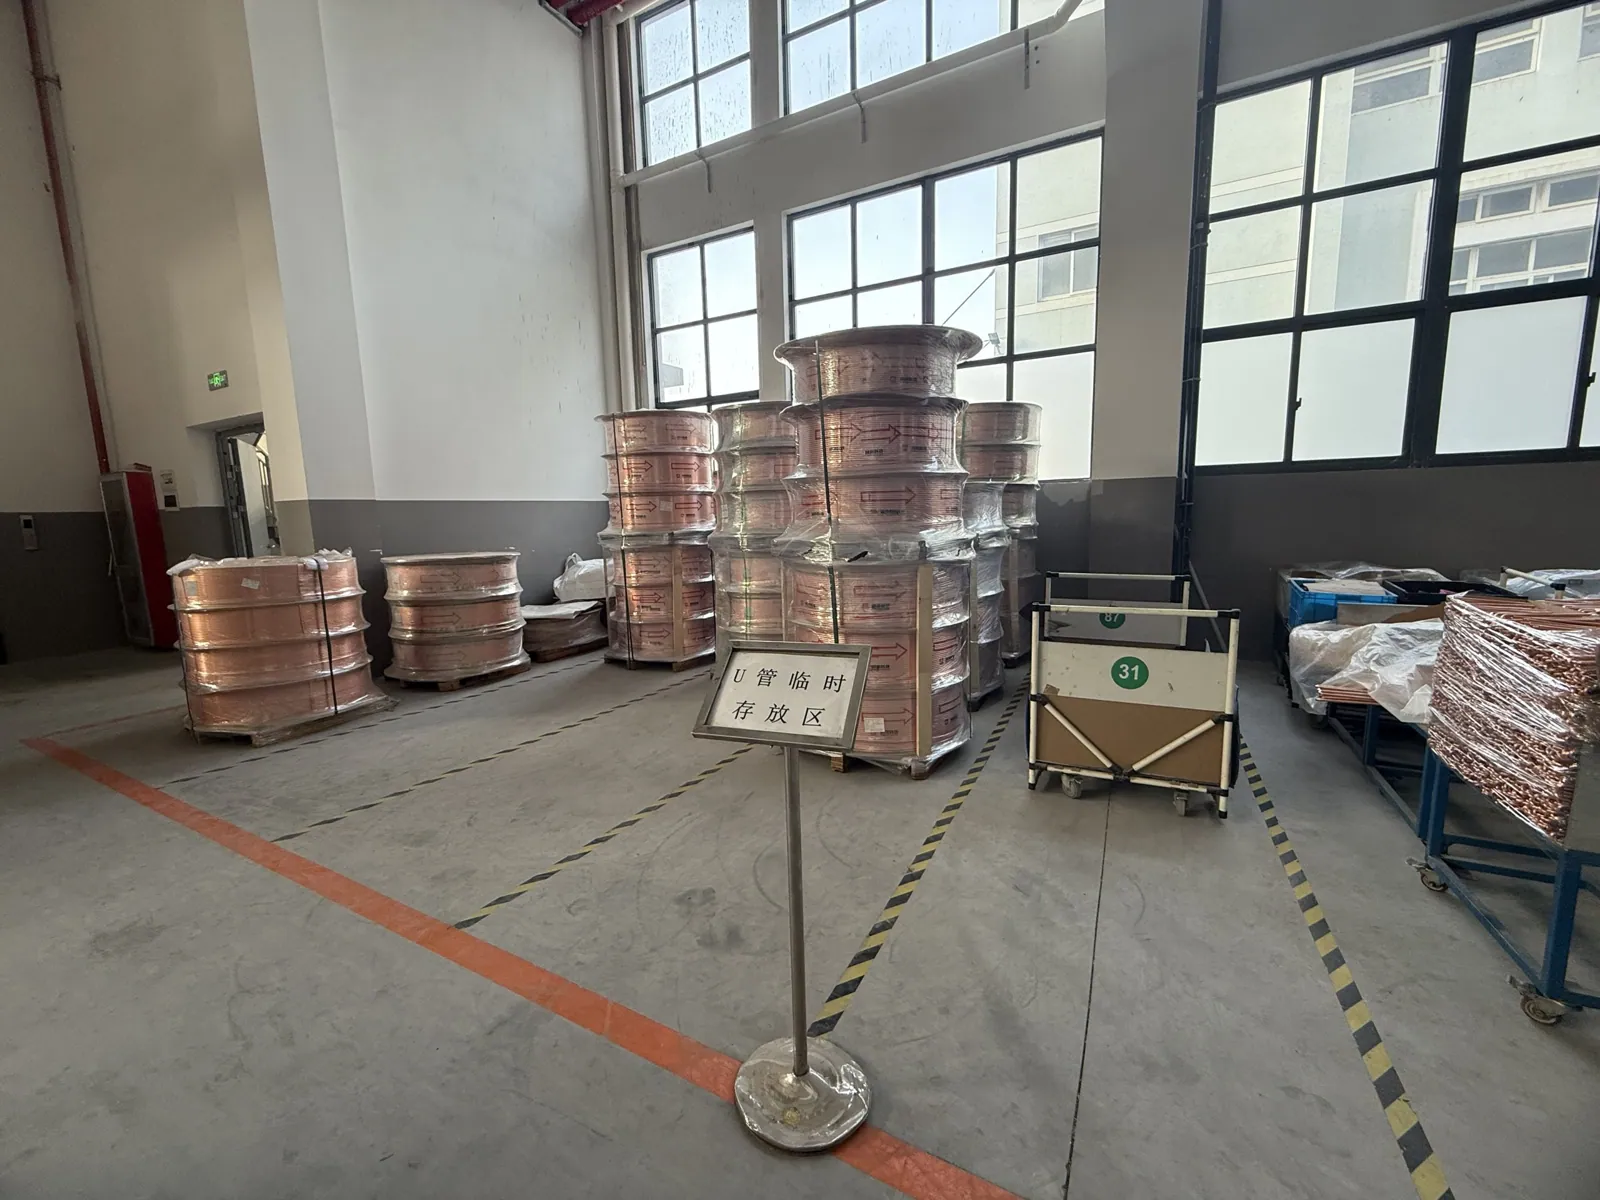
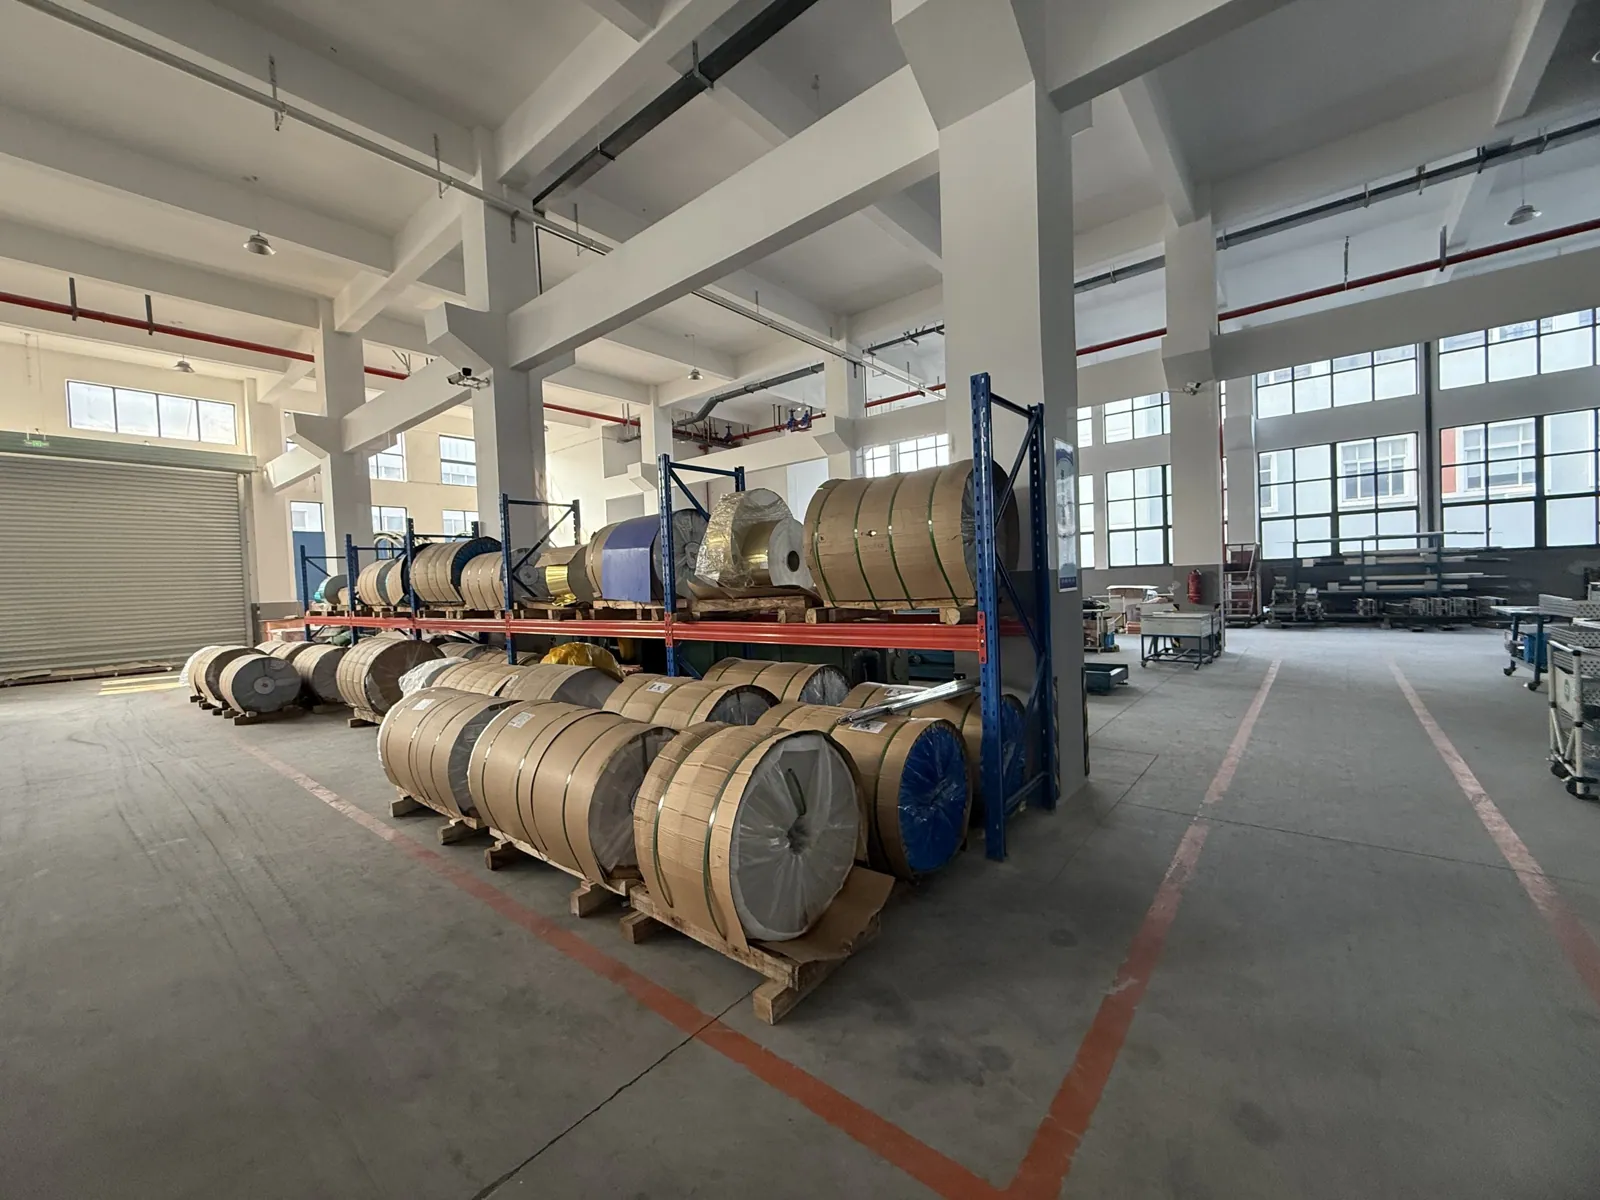
Reels of copper tube in the material store
Copper tube. TP2M inner-grooved tube, 7 to 15.88 mm outside diameter.
Coils of aluminum fin stock
Aluminum fin stock. 8011-H24 foil, hydrophilic, bare or anti-corrosion coated.

Other workshops

Cold boxes and refrigeration units are built on the same site.
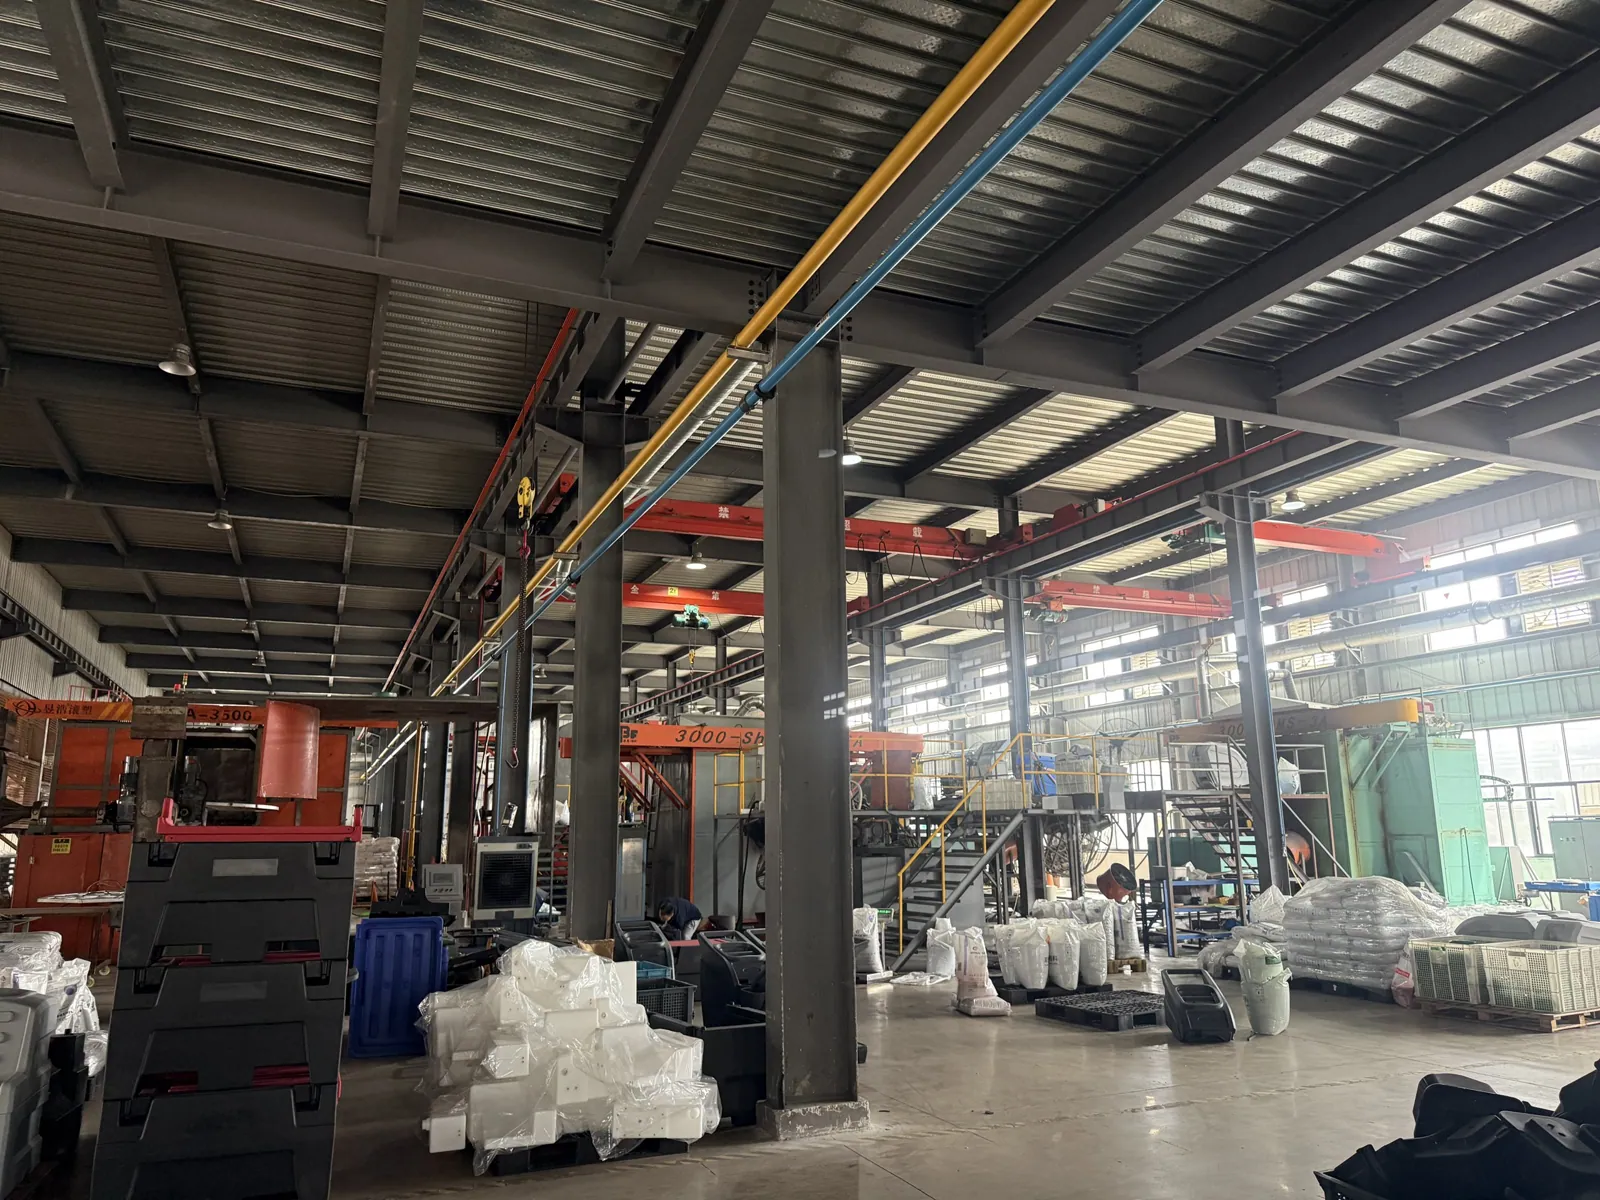
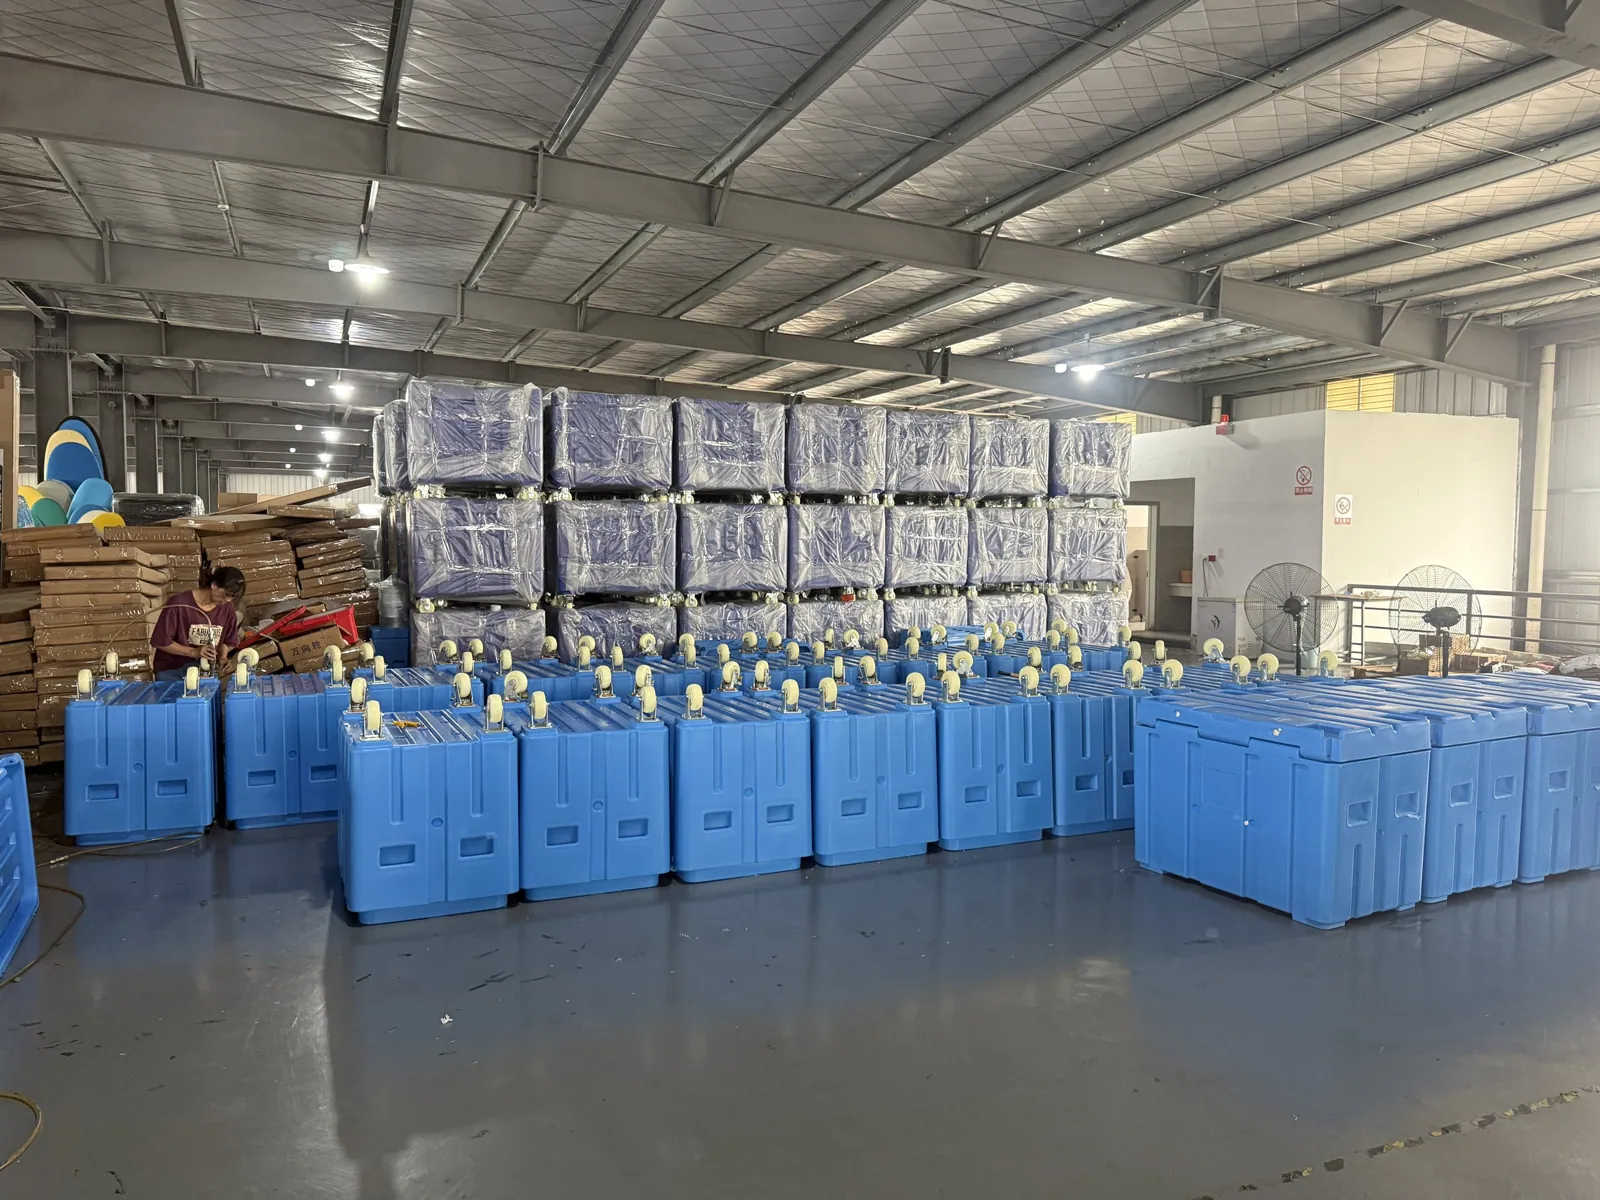
Rotational molding workshop with molds and finished shells
Rotational molding. Double-wall polyethylene bodies for the LMS980, fish tubs and cooler boxes are molded here and filled with polyurethane foam.
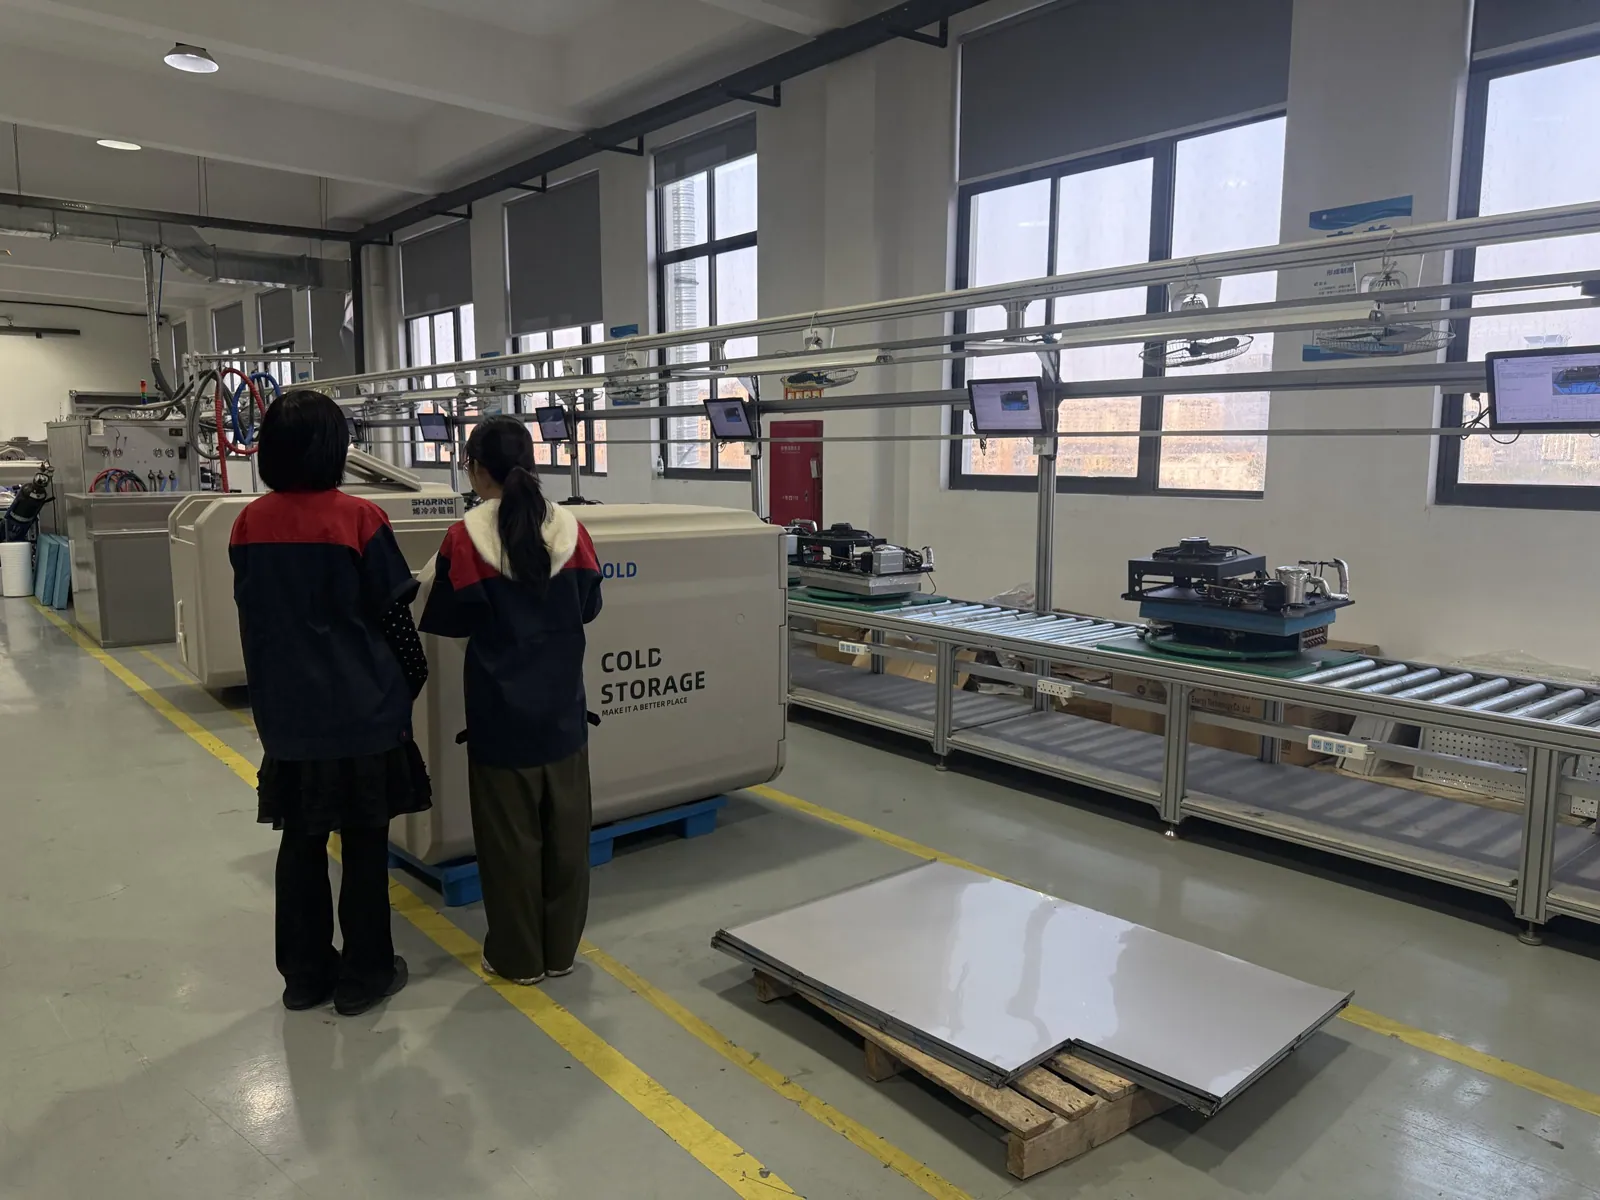
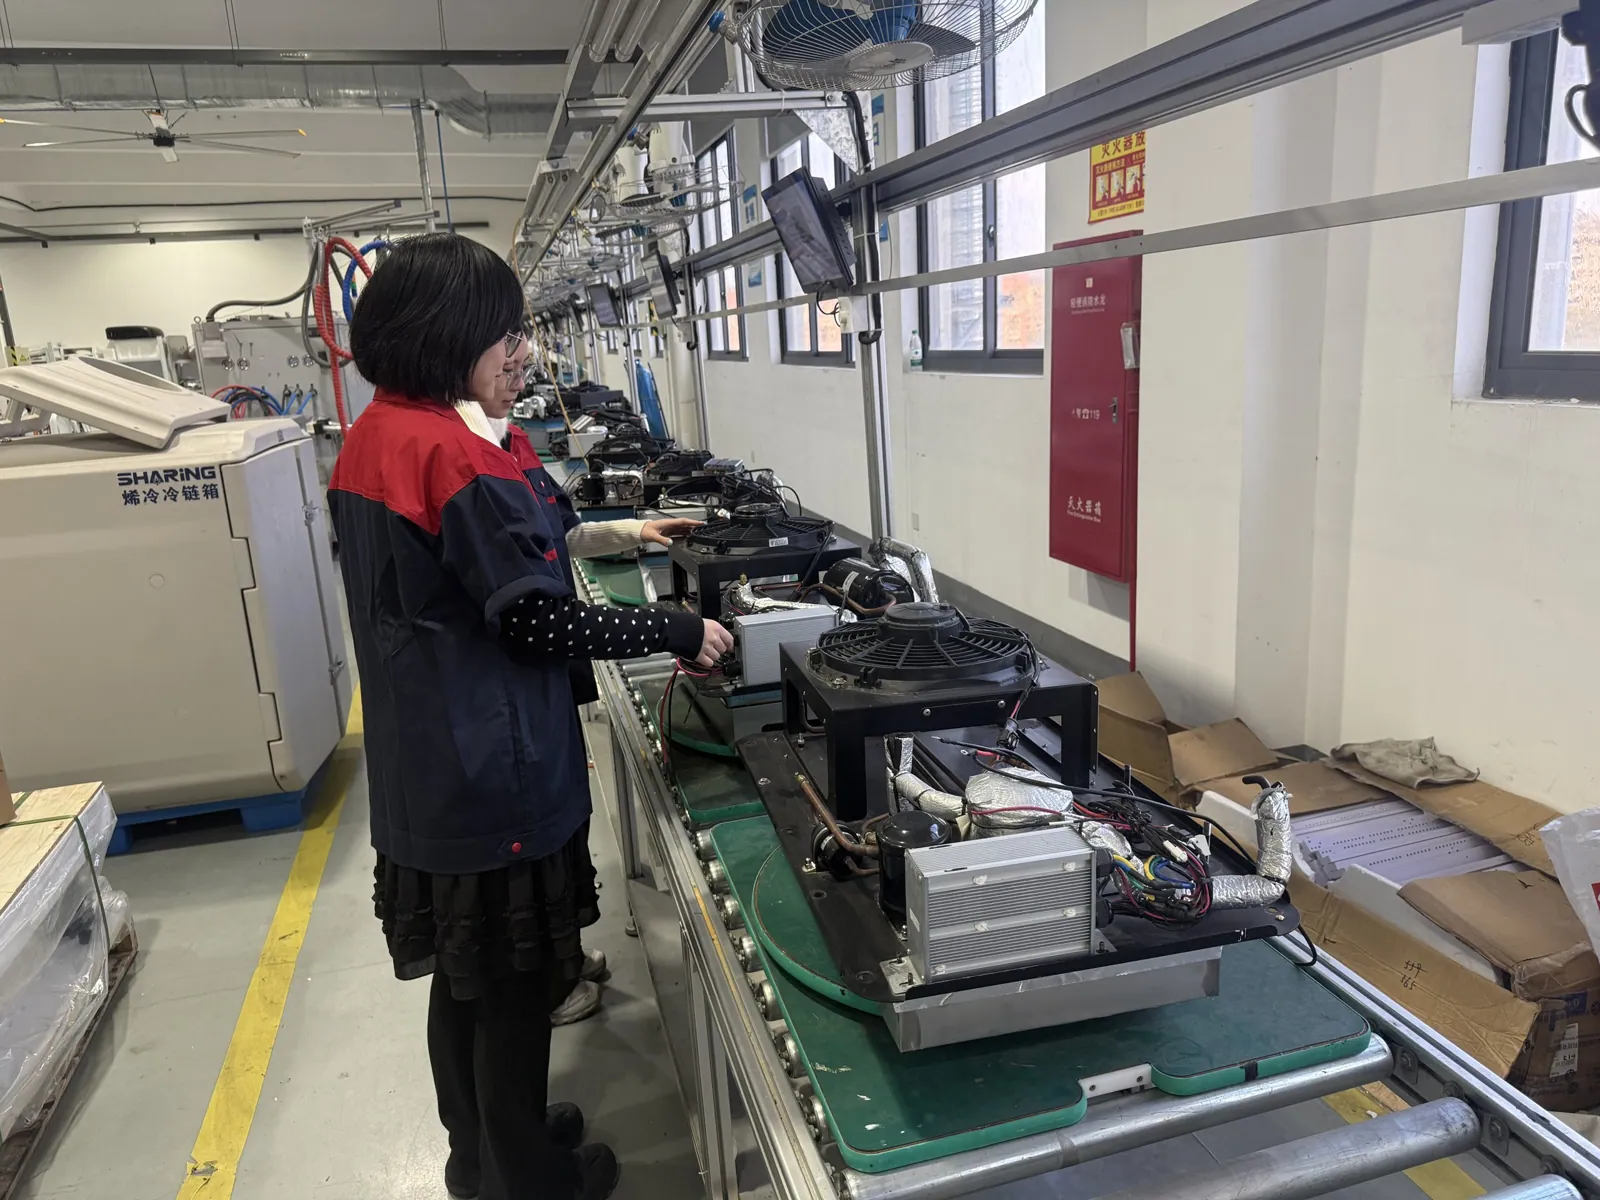
Refrigeration unit assembly line with workers at stations
Refrigeration unit assembly. Compressor units are assembled, wired and charged on a dedicated line.
Assembly line for finished refrigeration products
Final assembly. Units and bodies come together, and each finished product is checked before packing.
Workers assembling dry ice boxes
Dry ice box assembly. Insulated boxes for dry ice are assembled in their own area.

See it for yourself.

Visit the plant in Ningbo, or ask for a live video call from the production floor.

WhatsApp